China CNC Press Brake: What Makes It a Smart Choice for Metal Fabricators?
2026-09-19
What if the key to tighter tolerances and faster turnaround isn't a pricier machine, but a smarter sourcing decision? China's CNC press brakes have quietly evolved into precision workhorses, and HUNSONE is one name fabricators keep coming back to. Before you assume all options are the same, here's what sets this choice apart.
Precision Bending That Cuts Scrap and Rework
Every bend in sheet metal carries a hidden cost when angles drift by even half a degree. Scrap bins fill with near-miss parts, and rework hours eat into margins that once looked healthy. Our approach locks the bend sequence to the material's actual springback behavior, not a generic lookup table. By measuring each sheet's thickness and grain direction before the first stroke, the press brake adjusts in real time, so the first piece comes out right more often than not.
The difference shows up in the quiet moments on the floor—fewer trips to the grinding wheel, less sorting through discard piles for a usable prototype. Operators stop babysitting the backgauge and start trusting the machine to hold tolerance across a full batch. That trust comes from closed-loop angle correction that reads the bend as it happens, nudging the ram a few microns when needed, instead of relying on trial bends and hope.
What gets eliminated isn't just wasted steel. It's the phone call explaining why a job is late, the extra setup charge nobody planned for, and the nagging feeling that your equipment is fighting you. Precision bending done this way turns a cost center into a quiet profit engine, one accurate flange at a time.
How Chinese Manufacturers Keep Frame Costs Low Without Sacrificing Rigidity
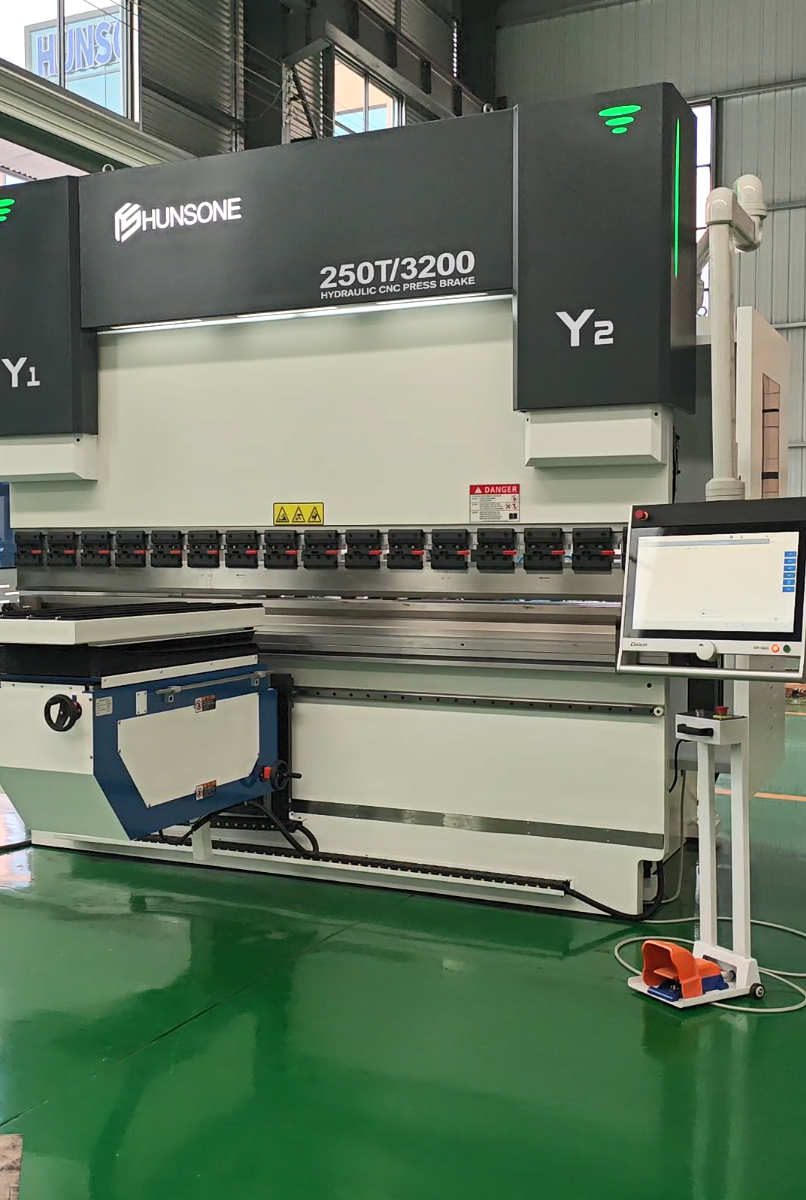
A key factor lies in the strategic use of high-strength low-alloy (HSLA) steels and precision roll forming. Instead of relying on thicker gauge material to achieve stiffness, Chinese factories often redesign cross-sections with deeper ribs and optimized flange geometry. This approach adds rigidity through shape rather than mass, allowing the frame to meet torsional targets while using less raw steel per unit. Pairing this with automated welding jigs ensures repeatable joint quality, which further stabilizes structural performance without the labour cost inflation seen in more manual production environments.
Another overlooked lever is vertical integration at the component level. Many manufacturers produce their own brackets, gussets, and mounting plates in-house rather than sourcing them from third-party stampers. This cuts logistics overhead and allows tighter tolerance control, which means less post-weld straightening and fewer rejected assemblies. The savings are then redirected into better corrosion-resistant coatings and closed-section reinforcement, so the final product doesn't just meet baseline rigidity – it often exceeds it under real-world loading conditions.
Finally, volume-driven tooling amortization plays a massive role. Chinese suppliers frequently run dedicated production lines for a single frame family, spreading die and fixture costs over hundreds of thousands of units. This lets them invest in more sophisticated multi-stage forming processes that would be prohibitively expensive for low-volume Western fabricators. The result is a frame that uses advanced shaping to lock in stiffness without premium material costs, challenging the outdated assumption that low price automatically means a flimsier structure.
CNC Controls That Turn Complex Setups Into a 5-Minute Job
A lot of shops still lose half a shift squaring vises, touching off tools, and double-checking work offsets. Modern CNC controls quietly erase that entire routine. The shift comes from how the interface handles probing cycles and tool measurement — what used to be a manual sequence of edge finders and test cuts is now a single canned cycle. The control reads the probe data, updates the coordinate system, and even flags any mismatch with the expected part geometry before the spindle starts turning.
The real difference is in conversational programming that actually feels like it was designed by machinists, not software engineers. Instead of writing G-code from scratch, you fill in a few fields on a touchscreen — hole pattern, pocket depth, thread pitch. The control then generates the toolpath on the fly, picks sensible feed rates, and orders the operations to avoid air cuts. It's closer to answering a short questionnaire than programming a machine.
For shops running repeat jobs or prototype work, the time savings compound quickly. You can store the entire setup recipe — probe points, tool lengths, fixture offsets — under a single part number. Next time the job comes around, loading that file brings the control back to the exact same state. A new operator can go from raw stock to a finished first article in about the time it takes to brew a coffee.
Custom Bed Lengths and Tooling Options With Faster Turnarounds
Standard machine beds rarely fit every job, so we build or modify bed lengths around your actual part dimensions. Short runs with small components get a compact setup that saves floor space and improves rigidity, while long shafts or rails can run on extended beds without awkward repositioning. You decide the working envelope instead of adapting your design to a fixed machine.
Tooling options go beyond the usual catalog. We keep a range of quick-change holders, multi-axis heads, and custom form tools ready for immediate use, which means less waiting on special orders. If a particular material or profile needs a different cutting geometry, we can grind or source the tooling in-house and test it on your setup before production starts.
That combination of tailored bed length and ready tooling removes much of the delay typically caused by machine reconfiguration. Because we don’t outsource these adjustments, turnaround times stay short even for non-standard geometries. You get a machine configured for your job, not a workaround that adds extra steps and cost.
Hydraulic Systems Designed for Three-Shift Production
Running hydraulic equipment around the clock exposes every weak point in the circuit—heat buildup, seal fatigue, and valve drift don't wait for a convenient shift change. Systems engineered for three-shift operation start with oversized reservoirs and forced cooling loops sized for continuous duty, not the intermittent peaks of a single-shift schedule. Filtration is doubled or tripled in parallel, with differential pressure indicators placed where a maintenance walk-by will actually see them. The goal is not to make breakdowns impossible, but to make the first sign of trouble visible hours before it becomes a line stoppage.
Component selection shifts dramatically when uptime is measured in 144-hour weeks. Cylinders get hard-chromed rods and scraper seals rated for millions of cycles, while pumps are chosen for slow-speed, high-volume operation rather than maximum pressure spikes. Manifold blocks are machined from solid billet to eliminate internal leakage paths, and every solenoid valve is specified with a manual override so troubleshooting can happen without disabling the entire circuit. Accumulators are sized to hold pressure during brief pump changeovers, turning what would be a full shutdown into a five-minute swap.
The real difference appears in the control architecture. Three-shift hydraulic power units run on load-sensing variable displacement pumps tied to a PLC that watches cycle times and pressure trends. If a clamp cylinder starts taking an extra half-second to build pressure, the system flags it for scheduled maintenance before the night crew ever notices a slow leak. This predictive approach, combined with quick-connect test points at every major branch, means the midnight shift spends its time making parts, not chasing pressure drops through a dark machine hall.
Overseas Support That Actually Answers Before Your Line Stalls
Calling overseas support usually means watching the minutes tick by while a robotic voice promises "your call is important to us." Here, the phone rings twice — maybe three times — and a real person picks up, already looking at your account. No labyrinth of menu options, no hold music that loops into eternity. Just a direct line to someone who can actually fix the problem.
The difference is in the setup. Instead of routing every international call to a central queue that's perpetually swamped, the network distributes queries to regional specialists who aren't juggling fifty tickets at once. That's why you won't hear "all our agents are busy" — because capacity is matched to demand, not squeezed for cost savings. A callback option exists, but it's rarely needed.
Even better, the people you reach aren't reading from a script. They're trained to troubleshoot, authorized to make refunds or adjustments on the spot, and fluent enough in the local context to understand why your payment failed in Manila or why customs held your parcel in Berlin. When support picks up before the line stalls, it's not just faster — it's actually useful.
FAQ
They now combine rigid welded frames, imported CNC controllers, and precision backgauges at a fraction of European prices. Many factories have improved their quality control and offer video inspections before shipment, so buyers can verify tolerance and bending repeatability before paying.
Look beyond the spec sheet. Ask about the brand of hydraulic valves, the type of linear guides, and the controller software version. Request a bending test on your own material thickness and a thermal stability report. A reliable supplier will share deflection compensation data and show the machine running a six-hour continuous test.
For mid-range and high-end models, the gap is minimal. Many use the same German or Japanese CNC systems, servo drives, and hydraulic manifolds. The key difference is often the level of hand-finishing and assembly consistency, which you can manage by choosing a manufacturer with ISO-certified assembly lines and documented calibration procedures.
Yes, customization is one of the strongest reasons to buy from China. You can specify additional axes, taller daylight, custom tooling, special safety light curtains, or even a different control interface. Unlike some larger Western brands that restrict modifications, most Chinese builders will adapt the machine to your production line without massive engineering fees.
Established exporters usually offer 24/7 WhatsApp or WeChat support, remote diagnostics, and spare parts shipped by air within days. Some have local service partners in major markets. Before ordering, confirm the warranty length on the hydraulic system and controller, and ask for a written response time guarantee—not just a promise.
Typically 30% to 50% compared to a similarly equipped European model. The savings come from lower labor and overhead costs in Chinese factories, not from using inferior parts. If you select a machine with imported hydraulics and a proven controller, the total cost of ownership over five years often beats the Western alternative.
Request a live video of the exact machine you will receive, not a demo unit. Ask for contact details of two or three current customers in your country. Check the warranty terms carefully—especially coverage for the CNC system, hydraulic pump, and backgauge ballscrews. A factory tour via video call can also reveal assembly practices and testing rigor.
Conclusion
Chinese CNC press brakes have moved past the old stereotype of cheap but flimsy machines. The precision bending on current models is tight enough to cut scrap and rework dramatically, which matters when you're running stainless or high-tensile plate. Frame costs stay low because fabricators use optimized welded structures and locally sourced steel, yet the rigidity holds up under full tonnage. Pair that with CNC controls that turn a complicated multi-bend setup into a five-minute job, and you get a machine that actually justifies its floor space.
What really tips the decision for many shops is the flexibility and uptime. Custom bed lengths and tooling packages ship with shorter lead times than most expect, so you aren't locked into a one-size-fits-all configuration. The hydraulic systems are engineered for three-shift production, with cooling and filtration that keep oil temperature stable through continuous cycles. And when something does need attention, the support teams from established Chinese builders tend to respond with actual technical answers instead of scripted troubleshooting. That combination of low purchase price, quick setup, and dependable backup is why so many metal fabricators now see a Chinese press brake as a practical, smart investment.
Contact Us
Contact Person: James Chen
Email: [email protected]
Tel/WhatsApp: 86 13770803946
Website: https://www.hunsone.com/