Custom Stainless Steel Casting Guide to Material Selection and Process Benefits
2026-10-18
Every stainless steel casting starts with a single decision: which alloy will survive the environment it’s about to face. From corrosion resistance to mechanical strength, the choice is rarely obvious—and the process behind it matters just as much. In this guide, you’ll learn how to match material grades to real-world demands and uncover the overlooked process benefits that separate a good casting from a great one. Whether you're optimizing an existing design or starting from scratch, the insights from Zhaoyuqi will help you make confident, cost-effective decisions without the usual guesswork.
How Alloy Chemistry Drives Corrosion Resistance in Stainless Castings
Chromium is the non-negotiable starting point. At levels above roughly 10.5%, it reacts with oxygen to form a transparent, self-healing oxide layer only a few atoms thick. But that film’s resilience depends heavily on what else shares the alloy. In a casting, uneven cooling can leave chromium tied up in carbides or intermetallic phases, so the effective chromium in the matrix—not just the nominal percentage—sets the baseline corrosion behavior. A well-designed chemistry keeps enough chromium in solid solution to repair the passive layer after scratches or thermal excursions.
Molybdenum and nitrogen quietly do the heavy lifting once chlorides enter the picture. Molybdenum disrupts pit initiation by stabilizing the passive film against aggressive anions, while nitrogen not only boosts pitting resistance but also slows the acidification inside growing crevices. Their combined effect is often approximated by the pitting resistance equivalent number, though real castings rarely behave exactly like wrought equivalents. Localized segregation during solidification can create micro-zones lean in these elements, and those are precisely where attack starts.
Nickel plays a more structural role, keeping the austenitic lattice intact so that other elements remain uniformly distributed. Carbon demands careful control as well—too much, and chromium gets pulled out of solution as chromium carbides along grain boundaries during slow cooling in the mold. That leaves adjacent regions depleted and vulnerable to intergranular corrosion. Adjusting chemistry to favor low carbon or adding stabilizing elements like titanium or niobium changes the precipitation sequence, preserving corrosion resistance even in thick sections that cool slowly.
Matching Stainless Grades to Temperature, Wear, and Chemical Exposure
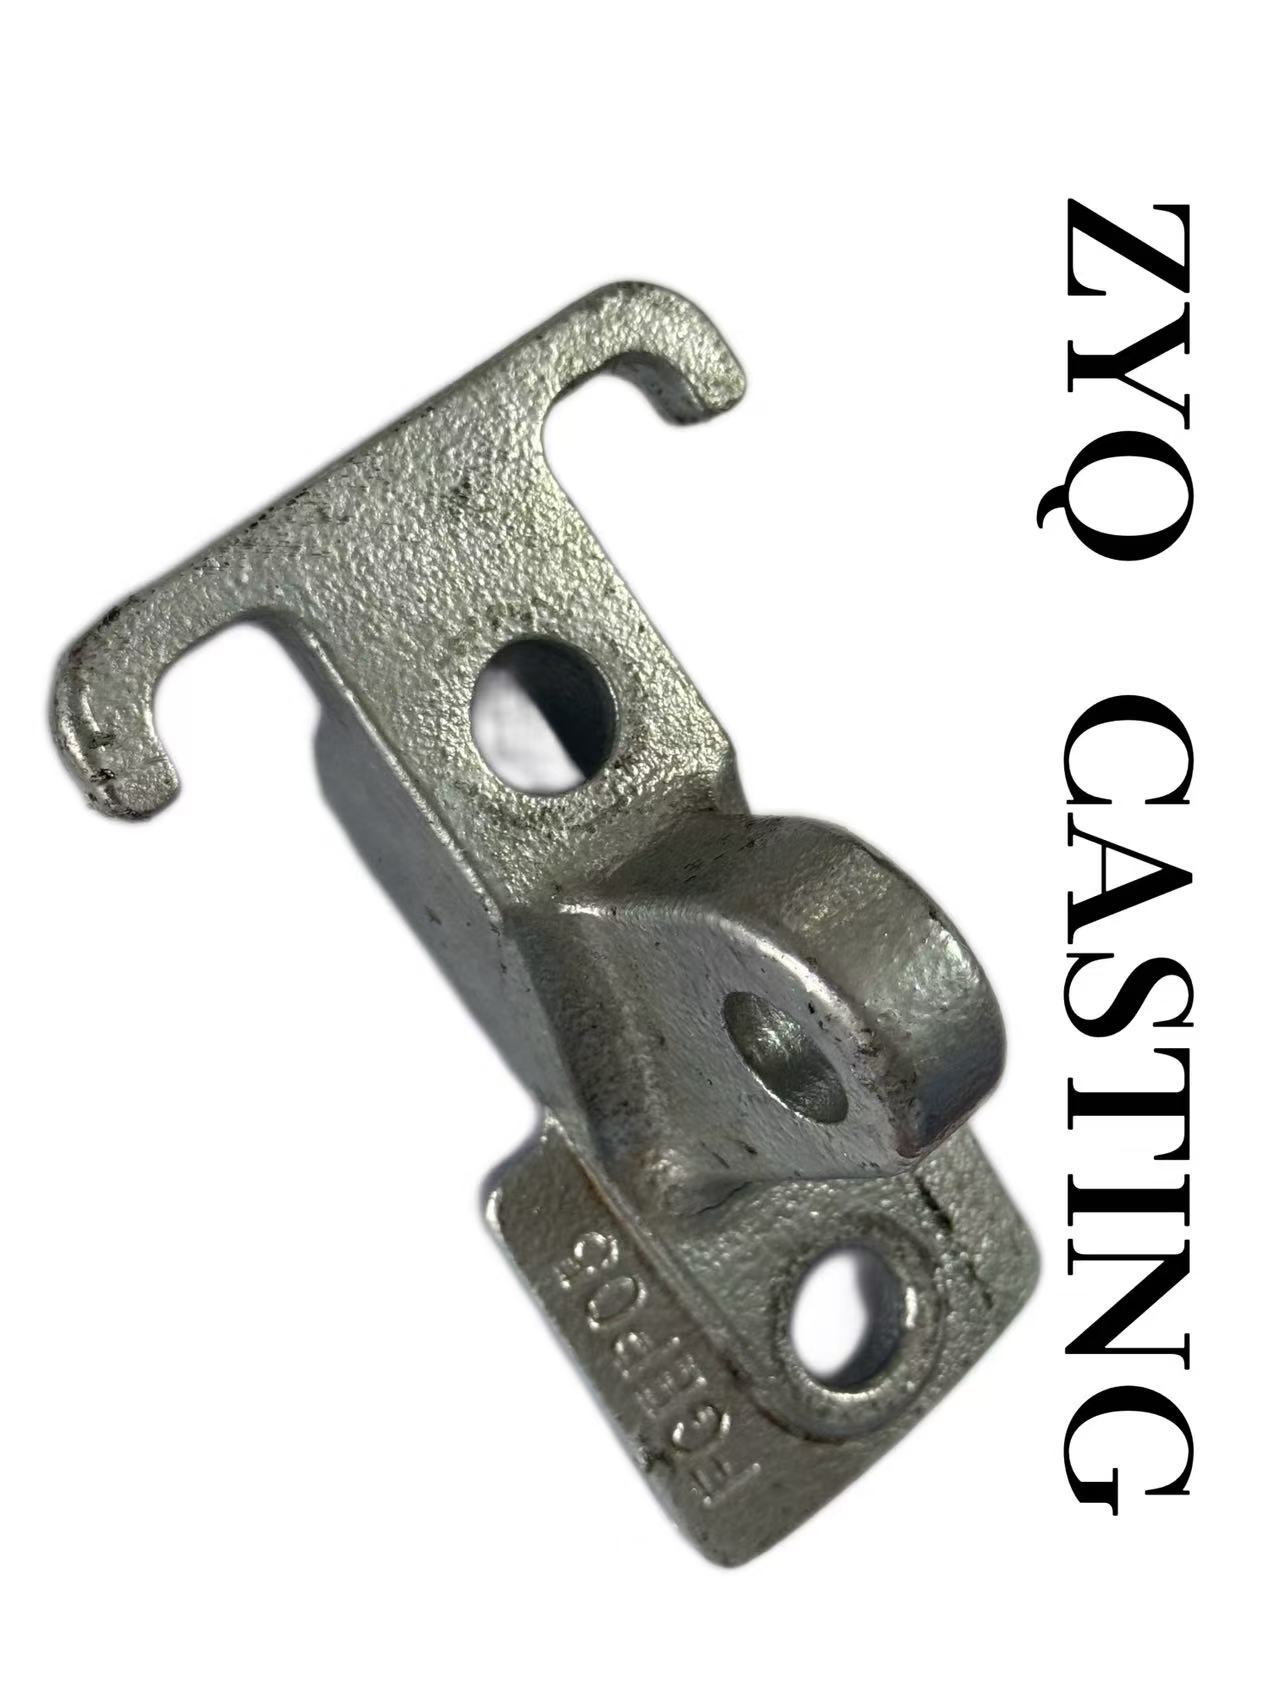
Selecting a stainless grade rarely comes down to a single property. A part that handles hot dilute acids might seem fine on a corrosion chart, yet the same alloy can deform under modest load once temperatures climb. 316L, for example, offers decent chemical resistance and holds up in many process environments, but its creep strength falls off noticeably above 600°F. If the application also involves sliding contact or abrasive media, the surface hardness of the as-annealed material becomes the limiting factor rather than the bulk composition.
Wear resistance pushes the decision toward martensitic or precipitation-hardening grades. 17-4 PH can be aged to useful hardness while retaining better corrosion resistance than 440C, though it still trails 316L in strong chloride service. Duplex grades like 2205 split the difference when both pitting resistance and mechanical fatigue matter, but they are not immune to galling unless one surface is treated or a dissimilar mating material is chosen.
Chemical exposure tends to dominate the final call. In oxidizing acids, molybdenum-bearing austenitics such as 317L or superaustenitic 904L resist localized attack far longer than standard 304. Yet those same alloys may fail quickly in reducing conditions where a higher nickel content or a completely different family is required. The practical approach is to rank the three constraints—temperature, wear, and chemical attack—by severity for the specific component, then test the shortlisted grades under the actual operating cycle rather than relying on generic compatibility tables.
What Near-Net Shape Casting Does to Your Machining Budget
The most obvious shift is in roughing time. Near-net castings arrive with only a thin envelope of material left for final cuts, so the machine is no longer reducing a solid block to a skeleton. That single change pulls down tooling spend, coolant use, chip disposal, and spindle hours together. Complex profiles and internal passages that would require long reach tools and multiple setups become much cheaper to finish when the casting already holds the basic shape.
But the savings can leak away if the shop has to fight the casting for repeatable datums. A raw cast surface rarely gives the same clean reference as a ground billet, and if the foundry and machine shop don't agree on pick-up points, probing and re-clamping can eat into the gains. It helps to design cast datums on surfaces that won't be machined, or to leave small machined pads specifically for locating.
For higher volumes or costly alloys, the math tends to favor near-net even after accounting for tooling and setup. Roughing a titanium bracket from plate might take an hour, while the same part from a casting needs only ten minutes of semi-finishing and a few finish passes. The freed-up machine time often covers the cost of the casting die faster than expected, especially when you're already running at capacity.
Why Grain Structure in Cast Stainless Steel Beats Wrought Alternatives
When you pour molten stainless steel into a mold, the metal freezes slowly from the outside in. That sluggish cooling gives atoms time to arrange themselves into coarse, equiaxed grains—roughly the same size in every direction. Wrought stainless steel takes a different path: it’s mechanically worked, rolled, or forged, which stretches those grains into long, flattened bands. In many applications, that directional grain structure is a weakness wearing a strength’s clothes. It makes wrought material tougher along the rolling direction but noticeably weaker across it, like splitting firewood along the grain versus against it.
Cast stainless steel doesn’t play favorites with direction. Its random grain orientation means mechanical properties stay consistent whether stress comes from tension, compression, or torsion. That uniformity matters in pump casings, valve bodies, and marine hardware—parts that rarely see a single, predictable load path. Wrought alternatives can crack or delaminate when forces hit perpendicular to their grain flow, a failure mode you won’t find in a well-designed casting. The equiaxed structure also handles thermal cycling better, resisting the kind of intergranular stress corrosion that plagues elongated grain boundaries in wrought parts exposed to chloride-rich environments.
There’s another quiet advantage: cast grain structure creates microscopic tortuosity. Cracks that start in one grain must constantly change direction to move into the next, burning energy at every boundary. Wrought material’s aligned grains offer straighter, easier fracture paths. This is why cast stainless impellers survive cavitation damage longer than their forged counterparts, and why cast fittings often outlast wrought ones in cyclic pressure service. You don’t need a lab test to see it—just compare the broken surface of a cast part’s jagged, rocky fracture to the smooth, layered split of a wrought piece pulled apart across its grain.
Design Geometries That Only Custom Casting Can Deliver
Most standard manufacturing routes force you to accept straight lines, uniform walls, and simple hollows. Custom casting breaks that mold. It lets you blend sweeping curves with abrupt bosses, transition thick sections into thin webs, and bury complex internal passages where no drill or weld could ever reach. The geometry isn't just an aesthetic choice—it determines how load paths flow, how heat dissipates, and how the final part survives in the field.
Think of a pump housing that wraps a spiral volute around an offset impeller, or a structural bracket that merges mounting lugs, cooling fins, and a cable chase into a single pour. These shapes aren't assembled from pieces; they emerge as one continuous grain structure. That continuity eliminates leak points, reduces stress concentrations at joints, and often lets you delete fasteners and secondary machining steps entirely.
When the design calls for a form that subtractive methods would chew into scrap or fabricated assemblies would turn into a patchwork, custom casting becomes the only sane answer. The foundry doesn't care if your cross-section changes every inch or if the core needs to snake through three axes. If you can model it, a carefully engineered mold can often reproduce it—turning what looks like an impossible geometry into a routine pour.
When One-Piece Castings Eliminate Leak Paths and Assembly Headaches
Every bolted joint, gasket, or weld seam in a multi-part assembly is a potential leak point waiting to surface under pressure, vibration, or thermal cycling. A one-piece casting removes those failure modes entirely by forming the entire component from a single pour of metal. There are no interfaces to align, no seals to compress, and no fasteners to torque. In hydraulic manifolds, pump housings, and valve bodies, this monolithic approach consistently outperforms fabricated counterparts in long-term leak testing, simply because there is nowhere for fluid to escape.
Beyond sealing integrity, consolidating multiple parts into one casting transforms the assembly floor. Inventory counts drop, part numbers shrink, and the sequence of joining, aligning, and tightening disappears from the work instructions. What used to take three technicians and a tray of loose hardware now becomes a single pick-and-place operation. The time saved on assembly often offsets the higher upfront tooling cost within the first production year, especially for moderate to high volumes where repeatability matters.
Designers sometimes hesitate to move to a one-piece casting because of perceived limitations in internal geometry or material choice. But modern foundry techniques such as 3D-printed sand molds and investment casting have largely erased those barriers. Complex internal passages, undercuts, and thin walls are now routinely cast to near-net shape with minimal machining allowance. When the geometry is right, a single casting does more than reduce leaks and assembly steps — it quietly improves product consistency, lowers total cost, and gives the end user one less thing to worry about.
FAQ
Start with the expected chloride exposure and temperature. 316/316L works for many coastal applications, but if you have constant wet-dry cycling or chlorides above roughly 500 ppm, move toward 2205 duplex or 904L. Also consider whether the part will be welded, because low-carbon versions like 316L resist sensitization far better after welding.
Casting lets you combine several machined or welded pieces into one near-net-shape component. That removes most of the welding labor, fixturing, and scrap from machining. For parts with internal passages or odd geometries, casting often becomes cheaper once annual quantities exceed 50 to 100 pieces, even after accounting for tooling.
303 and 303Se are easy to machine but give up some corrosion resistance and weldability. If you want a balance, 416 works for moderate corrosion environments, while controlled solidification and calcium treatment can make 304L and 316L much friendlier to cutting tools. For higher strength with reasonable machinability, 17-4 PH is a solid choice after proper heat treatment.
Investment casting can produce walls down to 1.5–2 mm with tolerances around ±0.1–0.15 mm, but you need uniform sections and proper gating. Thin areas tend to warp or develop shrinkage porosity during cooling, so leave machining allowance on critical mating surfaces instead of expecting the raw casting to hit final precision.
Grain size and orientation directly affect yield strength, toughness, and stress-corrosion resistance. Coarse columnar grains can create weak planes and microcracks, especially in pressure-containing parts. Controlling pour temperature, using grain refiners, or switching to centrifugal casting produces a finer, more uniform grain structure that behaves more predictably in service.
Investment casting typically lands around Ra 3.2–6.3 µm, while sand casting is closer to Ra 6.3–12.5 µm. With a fine ceramic shell and careful primary slurry control, you can push investment castings to Ra 1.6–3.2 µm. Mirror-like finishes still require mechanical or electropolishing because the casting process alone cannot reach that level.
Choose 2205 duplex when the fluid has high chloride levels, temperatures above 40°C, or a real risk of crevice corrosion. It outperforms 316 in pitting and stress-corrosion cracking resistance. The trade-off is that duplex flows less easily during casting, needs stricter solution annealing, and wears cutting tools faster during machining.
Yes, significantly. Martensitic grades like 410, 420, and 440C are often hard and brittle in the as-cast state. They need normalizing or annealing to refine the structure, followed by quenching and tempering to reach the target hardness and toughness. Austenitic grades usually only require solution annealing to dissolve carbides and restore corrosion resistance, with little room to adjust hardness.
Conclusion
The real work in custom stainless casting starts long before the first pour. It begins with alloy chemistry—how chromium, nickel, molybdenum, and nitrogen interact to form a passive oxide layer that shrugs off pitting and crevice corrosion. But corrosion resistance isn't a single number. A grade that holds up fine in mild chemical splash may fail quickly in hot chloride service or under sliding wear. So the selection process becomes a balancing act: temperature limits, abrasive conditions, and the specific corrosive agents all pull you toward different stainless families, from austenitic 304/316 to duplex or precipitation-hardening grades. What's often overlooked is that cast stainless brings its own microstructural advantages. Unlike wrought bar or plate, a casting's grain structure follows the part's contours, which can mean better resistance to stress corrosion cracking in complex shapes. That's not a marketing claim—it's a direct consequence of how the metal solidifies in a mold.
Once the right alloy is locked in, the process benefits start compounding. Near-net shape casting dramatically reduces machining time because you pour metal only where the final part needs it, not where a mill cut it from a rectangular block. This is where custom geometry pays off: internal passages, variable wall thicknesses, and organic curves that would be impossible or wildly expensive to machine from solid. And when you cast a complex assembly as a single piece, you eliminate the gaskets, welds, and bolted joints that create leak paths and future maintenance headaches. Fewer joints mean fewer opportunities for failure under thermal cycling or pressure fluctuation. In short, a well-designed stainless casting doesn't just replace a fabricated or machined component—it changes how the part behaves in service, often with a lower total cost than the sum of its alternative parts.
Contact Us
Contact Person: Nico Yin
Email: [email protected]
Tel/WhatsApp: 8618561567088
Website: https://www.ductileironparts.com/