High Tenacity Polyester Filament Yarn Manufacturer: How to Evaluate Quality and Performance
2026-09-24
Buying high tenacity polyester filament yarn isn't just about matching a data sheet. If you've ever had a batch pass initial testing but fail weeks later in the field, you know the real test is consistency under stress. In this post, we'll walk through the evaluation steps that matter most — and why Changshu Polyester treats every quality check as a non-negotiable part of production.
Real Strength Is More Than a Denier Number: Specs That Separate Premium Yarn
Denier gets treated like a strength rating, but it only tells you how heavy the fiber is—not how well it survives real use. A 40-denier nylon can snap under less load than a well-spun 20-denier polyester if the latter has longer staple fibers, higher tenacity, and better elongation before break. Premium yarns are specified by grams per denier, not just denier alone, because that ratio shows how much force each strand actually carries. Fiber length matters just as much: long staples twist into place with fewer loose ends, so stress spreads across the yarn instead of concentrating at weak points.
The details that separate premium yarn from commodity stock usually don't appear on a hangtag. Twist level, ply balance, and abrasion resistance do more to prevent failure than a bigger denier number. Too much twist makes yarn stiff and prone to cutting itself under load; too little lets filaments slip. Balanced multi-ply construction evens out torque and fills in thin spots, which is why two yarns with the same denier can feel completely different on a pack. Abrasion testing, not just tensile pull, shows whether the yarn will survive rubbing against hardware or sharp gear edges.
Consistency is the quiet spec that matters most. Premium yarn carries tight tolerances for evenness and defects like slubs or knots—every weak point is a future break. Moisture regain and heat resistance also play in: high-end technical yarns keep their strength when wet or near hot pack frames instead of turning brittle. Next time a label leans hard on a denier count, ask what it doesn't say about twist, staple length, and per-filament toughness. That missing data is where real durability lives.
Polymer Purity and Melt-Spinning Discipline: What to Verify First
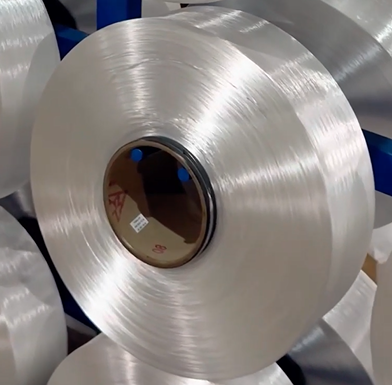
Before you even think about ramping up throughput or chasing finer deniers, grab a sample from the dryer and run a quick intrinsic viscosity check. It sounds basic, but a drop of 0.02 dL/g can quietly ruin your spinline stability. I've seen operators blame everything from spinneret design to quench air turbulence when the real culprit was a bag of resin that had been sitting open in a humid warehouse for three days. Moisture and hydrolytic degradation don't announce themselves with a bang—they just make your filament break randomly at 2 a.m.
Next, look at the melt filter pressure trend over the last two shifts. A slow, steady climb that doesn't flatten out usually means you've got gel particles or degraded specks coming through. Don't wait for the pressure alarm; pull a filter screen and flatten it under a bright light. If you see tiny fisheyes or discolored flecks, stop the line and purge. Pushing through contaminated polymer just moves the problem downstream to your pack life and final fiber tenacity.
Finally, verify that your drying hopper's dew point is actually below -40°C and that the residence time matches the resin manufacturer's curve. I know it's tempting to shorten drying to keep production moving after a late resin delivery, but that shortcut shows up later as weak spots in the draw zone and inconsistent elongation. A ten-minute check with a portable dew point meter beats a full day of troubleshooting broken filaments and scrapped spools.
Beyond Breaking Load: Elongation, Shrinkage, and Knot Strength Tests That Catch Weak Spots
Most specs stop at breaking load, but a material that holds a high peak force can still fail in the field by stretching too far under normal tension. Elongation testing pulls a sample at a controlled rate and records how much it lengthens before yield or rupture. The resulting strain curve exposes weak spots that a one-time break test hides—like low-stretch fibers that snap without warning or high-stretch materials that allow components to drift out of alignment.
Shrinkage tests look at what happens after the load comes off. Some cords and webbings recover their original length quickly; others stay stretched or shrink unevenly once tension cycles repeat or heat builds up. Measuring dimensional change after a set relaxation period or thermal exposure catches these slow, cumulative defects. A rope that loses just a few percent of length after repeated loading can loosen knots, shift anchor points, or create slack in a system that was once tight.
Knot strength testing ties the material into a standard knot, then pulls it to failure. The knot creates a stress concentration that mimics real-world use far better than a straight pull. Many fibers lose 40% to 60% of their rated strength at a knot, and brittle or notch-sensitive materials can fail suddenly at that point. Comparing knotted versus unknotted break values reveals whether a product is tough enough for rigging, rescue, or marine work—or just looks strong on a datasheet.
Batch Logs and Independent Lab Data: How to Spot a Manufacturer’s True Consistency
Batch logs often read like intimate diaries of a production line—raw, unfiltered, and occasionally messy. Unlike polished marketing claims, these records show exactly when a machine drifted out of tolerance, how operators responded, and whether that rogue batch was quarantined or quietly shipped. A manufacturer with genuine consistency will have logs that are detailed enough to be boring: time-stamped adjustments, clear pass/fail notations, and no convenient gaps around problematic dates.
Independent lab data acts as the second set of eyes that catches what internal logs might miss or soften. When you see results from an outside facility testing the same product over multiple production runs, the real story emerges. Discrepancies between a company's own QC numbers and the independent reports usually point to either sloppy testing at one end or, worse, selective reporting. True consistency lives in the overlap—when both datasets tell the same steady, unglamorous story of minor variation within tight limits.
To spot a manufacturer's actual consistency, ignore the average and chase the extremes. Look at the worst batch in a year of logs, then cross-check it against the independent lab's findings for that same period. If the outliers align and still fall within acceptable ranges, you're looking at a process under control. If the logs show smooth sailing but the independent data reveals spikes, someone is rewriting history. The most reliable sign of consistency is boring agreement between two sources that have no reason to flatter each other.
Surface Finish, Dye Pickup, and Lubricant Uniformity: The Overlooked Quality Filters
When production lines push for speed, surface finish often gets treated as a cosmetic afterthought. But a rough or inconsistent surface can silently sabotage later stages—dye pickup becomes patchy because microscopic peaks and valleys trap or repel color unevenly. The same irregularity disrupts lubricant distribution, leaving some areas over-wetted while others run dry. These aren't separate issues; they're three symptoms of one unfinished conversation between material and process.
Think of dye pickup as a lie detector for surface prep. If the substrate hasn't been conditioned to a predictable roughness range, no amount of dye concentration adjustment will compensate. The result is visible banding or mottling that only shows up after the part leaves the line—expensive to rework, impossible to ignore. Lubricant uniformity follows the same logic: too smooth and the film beads up; too rough and it wicks away into the valleys, leaving the peaks unprotected.
The practical fix isn't more inspection at the end; it's treating these three variables as a single quality filter earlier in the workflow. A quick profilometer check alongside a standardized dye swatch test and a simple lubricant spread test can catch misalignment before it becomes a reject pile. Teams that stop chasing each defect individually and start managing the underlying surface condition typically see fewer surprises in final QA—and fewer heated calls with the finishing department.
Can They Handle Your Downstream Process? Probing Technical Support and Custom Twists
Most suppliers look polished on the surface, but the real test starts when you need to integrate their product into an existing workflow. You might find that their technical support team reads from a script and has never actually run a bioprocess at scale. Ask them pointed questions: What happens when your harvest viscosity spikes mid-run? Can they walk you through a filter sizing change on the fly? A vendor that flinches at those details will cost you weeks of downtime later.
Customization is another area where promises rarely match delivery. Every downstream process has its quirks — a fragile protein, an unusual buffer matrix, a tight elution window. A good partner will not just say yes to a custom adapter or a modified resin chemistry; they will show you previous case studies where they solved a similar puzzle. If their answer is always “it depends on the sales contract,” you are likely dealing with a distributor, not a manufacturer.
Before you commit, request a pilot-scale trial with your actual feed material. Watch how their engineers respond to unexpected pressure drops or conductivity drift. The ones who can troubleshoot on a call and adjust parameters without waiting for a scheduled meeting are the ones you want on your side. Technology is important, but the human element behind it is what keeps your downstream process running when things go sideways.
FAQ
For most load-bearing applications, aim for a tenacity of at least 7.5 grams per denier, with serious candidates reaching 8.0 to 8.5. Elongation at break should sit between 12% and 18%, reflecting a balance between stretch and stiffness. If a supplier only mentions breaking load without denier or tex, ask for the specific tenacity calculation.
The extrusion temperature, quenching rate, and draw ratio all shape the molecular orientation. A slow, controlled quench combined with a high draw ratio produces longer polymer chains aligned along the fiber axis, which directly boosts tenacity. Inconsistent spinneret pressure or uneven cooling shows up later as weak spots and poor knot strength.
Request a full tensile test report from an independent lab, not just a manufacturer's in-house data. Key values include breaking tenacity, elongation at break, and initial modulus. For dynamic applications, also ask for cyclic fatigue or abrasion resistance results. ASTM D885 and ISO 2062 are both reliable references for filament yarn testing.
High tenacity polyester can still lose length when exposed to heat during coating or vulcanization. If dry heat shrinkage at 177 degrees Celsius exceeds 8%, the fabric may wrinkle or the rope may lose pre-tension. Always ask for shrinkage curves at the temperatures you actually process, not just a single value from a low-temperature test.
Be suspicious if the quoted tenacity is far above 9 grams per denier without a corresponding lab certificate. Also watch for vague language like 'high strength' without numerical values, or if the data sheet mixes breaking load from single filaments with yarn bundle strength. A credible supplier will share full test methods and batch numbers.
Request samples from three separate production lots, not just one golden sample. Measure denier, tenacity, elongation, and shrinkage on each, then calculate the coefficient of variation. A tightly controlled process usually keeps tenacity variation below 3% across lots. If the supplier cannot provide production lot data, expect surprises later.
The spin finish affects fiber-to-metal friction and can make the yarn run smoothly or cause snagging during weaving or braiding. Twist, even a low level like 30 to 60 turns per meter, improves inter-filament cohesion and handling. Ask about the finish type and whether it is compatible with your coating or adhesive system, because the wrong finish can ruin adhesion.
Conclusion
A reliable high-tenacity polyester filament yarn supplier rarely wins on denier alone. Premium grades distinguish themselves through a cluster of mechanical specs—tenacity, modulus, elongation at break, and hot-air shrinkage—that collectively determine how the yarn behaves under load and heat. Before any purchase order, ask for polymer purity certificates and details of the melt-spinning setup, because inconsistent chip quality or poorly controlled quenching produces weak spots that only appear later as broken filaments or uneven dye uptake. Request full test reports that go beyond breaking load: knot strength and loop strength, shrinkage at 177°C, and elongation curves can expose brittle or unstable yarn that a simple tensile test misses. Independent lab data from randomly selected batches, not just the manufacturer's own numbers, is the clearest window into true consistency.
Equally revealing are the overlooked surface attributes. A uniform lubricant film and consistent spin finish directly affect friction, static build-up, and how evenly the yarn picks up dye—problems that turn into costly reworks in weaving or knitting. Ask for coefficient of friction values, finish oil percentage, and dyeability tests on the exact denier you plan to run. Finally, probe how the manufacturer handles downstream realities: can they adjust twist, intermingle points, or package dimensions to match your warping or texturing equipment? A supplier that offers technical support, quick pilot runs, and custom finish formulations is far more valuable than one that hides behind a spec sheet. Judged together, these checks separate a vendor who merely meets a data sheet from a partner who understands your process.
Contact Us
Contact Person: CONNIE
Email: [email protected]
Tel/WhatsApp: 86-0512-53671634
Website: https://www.lida-yarn.com/